

Beyond the arc: technologies to cut Scope 1 emissions of EAF steelmakers
Analysis report · Transition Asia · November 2026
“Switching to electric arc furnaces does not solve the whole decarbonisation challenge. Reheating and annealing can account for 65–92% of the process’s Scope 1 emissions.”
Cleaner steel does not stop at the arc furnace
Automotive and construction buyers are asking steelmakers for supply chain-wide (Scope 3) emission cuts, so future competitiveness depends in part on climate action. Moving to EAF production on scrap steel or lower-carbon iron such as direct reduced iron (DRI) is one of the most viable near-term strategies, but efforts cannot stop there. Decarbonisation also matters in downstream steps such as rolling and heat treatment, which turn molten steel into sheets and long products.
This report outlines the emission profile of today’s EAF steelmaking process, then examines four technologies that can replace fossil fuels in downstream heating: electric heaters, plasma torches, hydrogen burners and RotoDynamic heaters. We compare their commercial readiness, energy performance and capital cost, and set out three steps for EAF operators.
Fuel, not electricity, drives Scope 1 emissions in an EAF mill
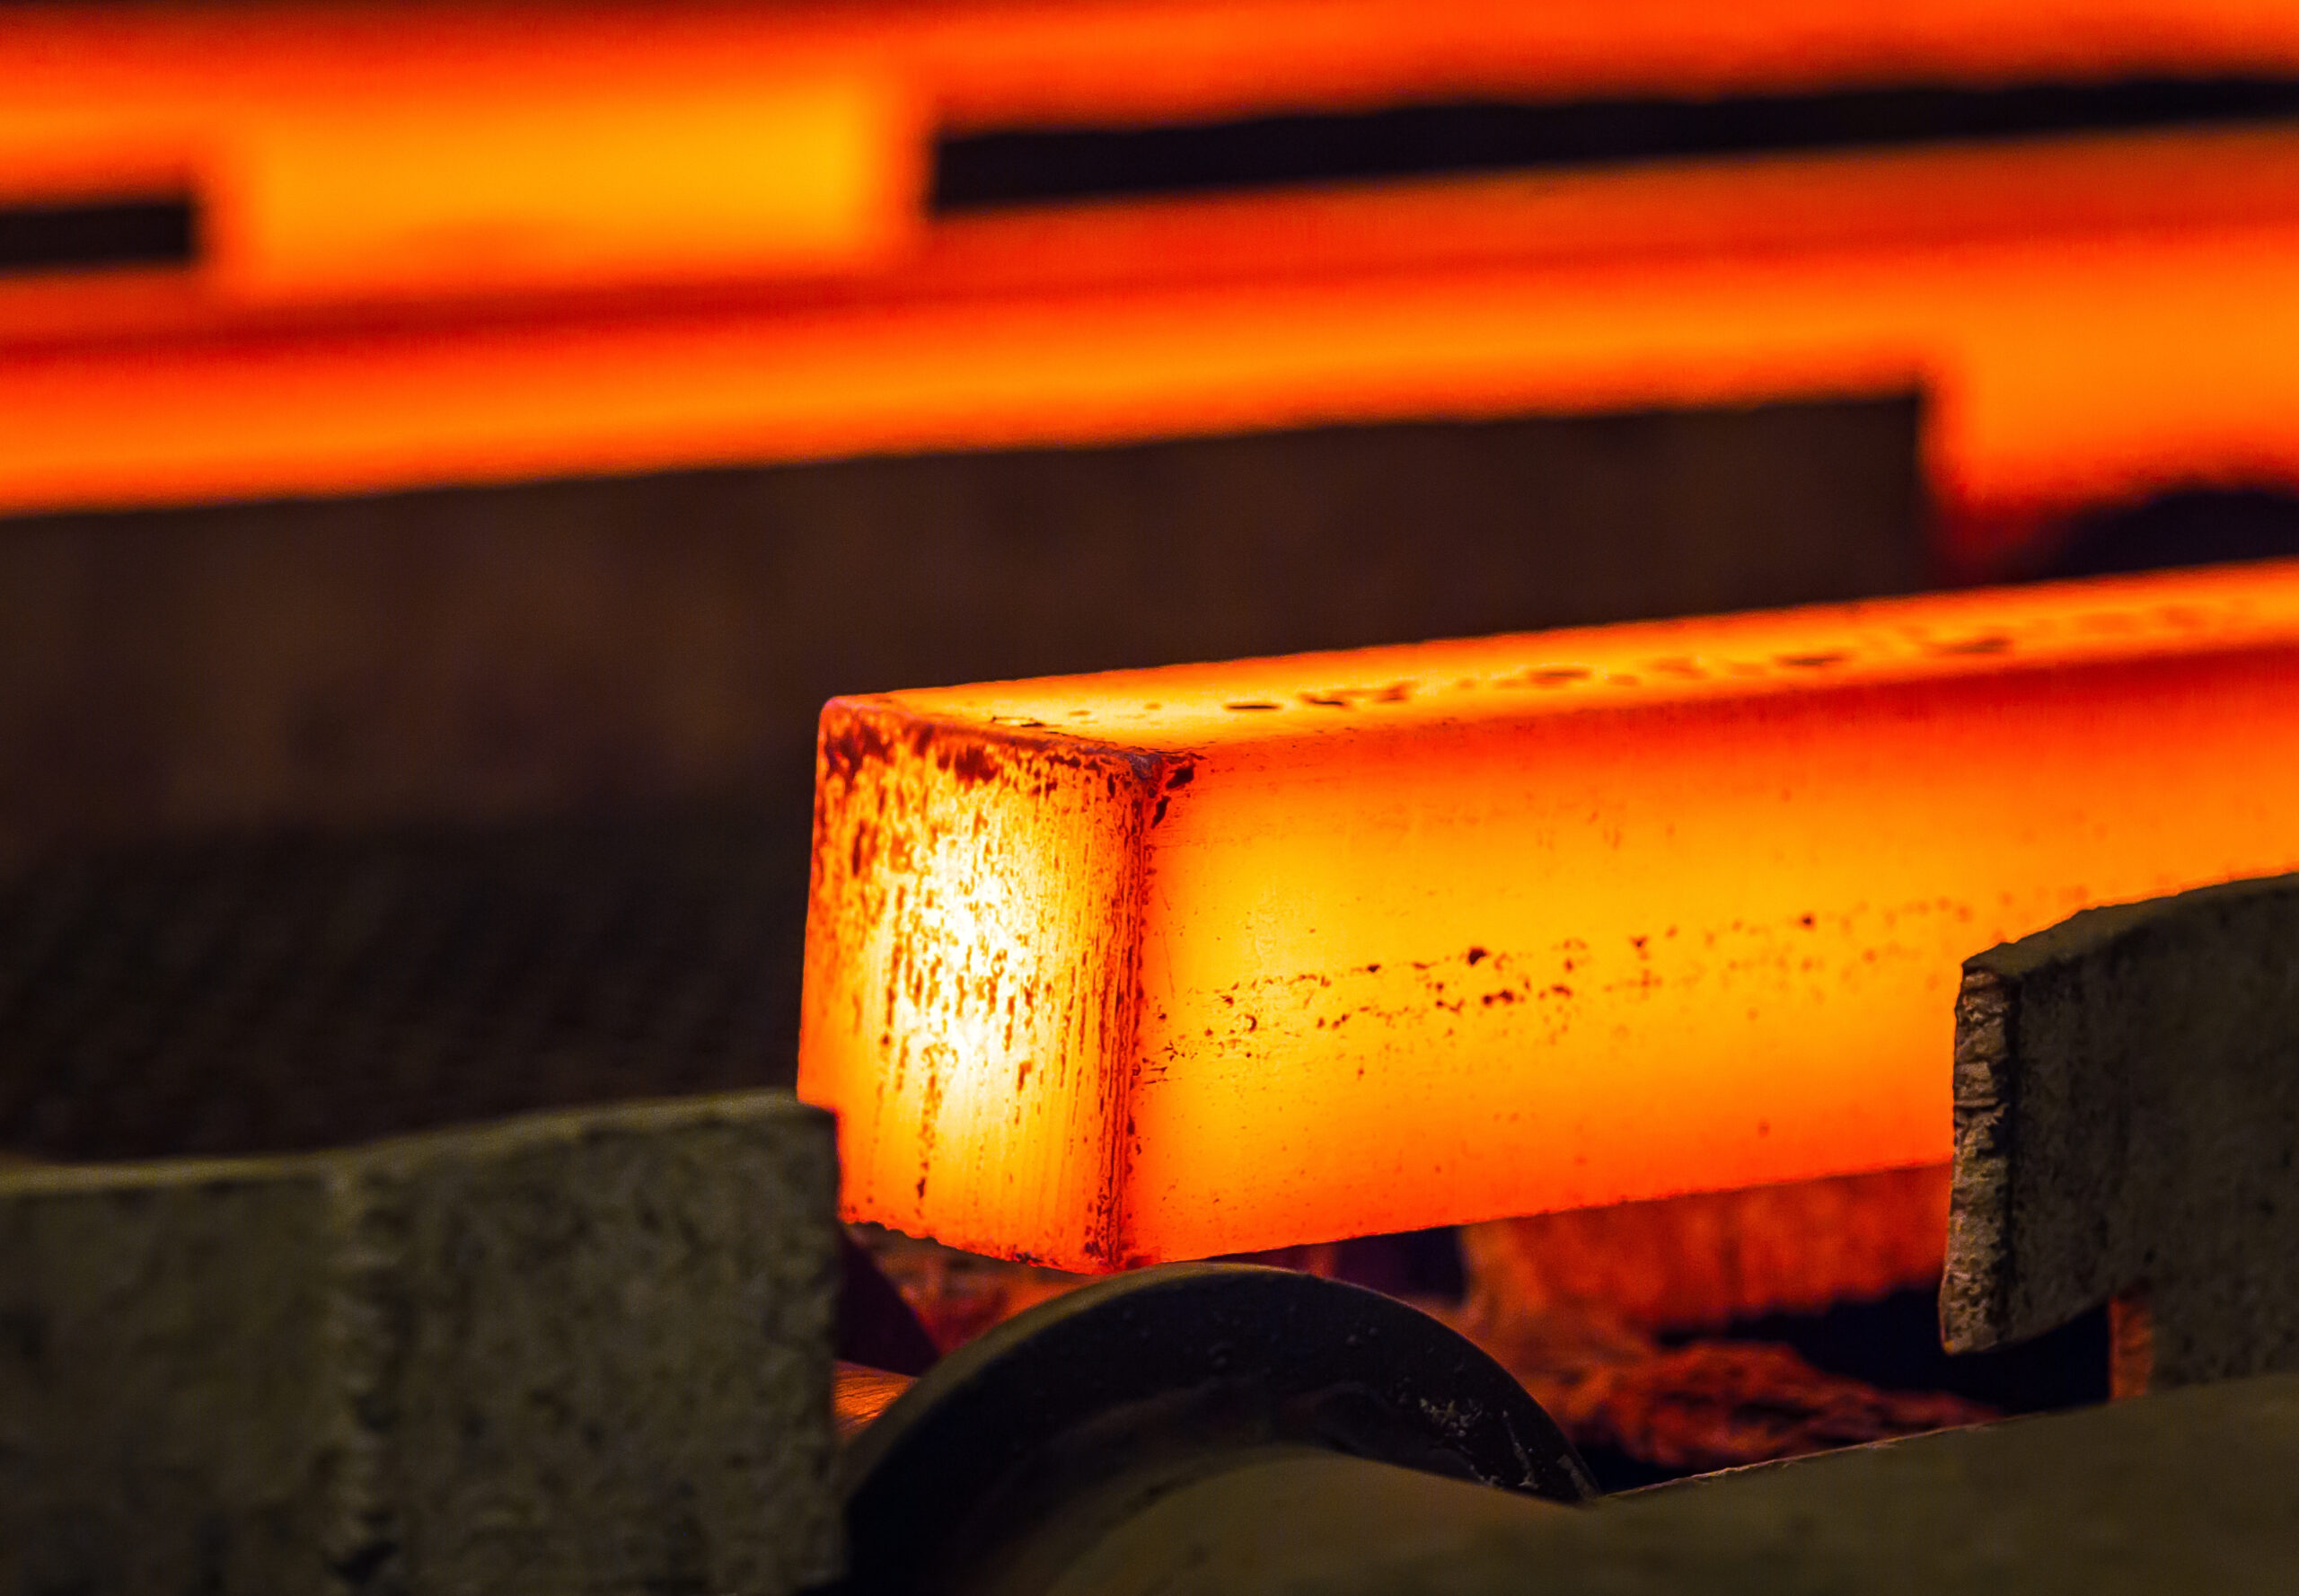
Two heating steps stand out on both fuel use and emissions: the reheat furnace and annealing.
Energy consumption and Scope 1 emissions by process
Key findings
Click a finding to open it.
Scrap-based EAF steel already emits far less than BF-BOF, but cleaner power does not finish the job
Reheating and annealing are where the Scope 1 emissions sit
Gas burners make EAF steel struggle to reach near-zero emissions
Four ways to replace the burners
Four technologies can replace the fossil-fuel burners in reheating and annealing, but they differ sharply in maturity, power demand and retrofit effort.
Readiness at a glance
Up to 95% thermal efficiency
Fully commercialisedPlasma jet up to 5,000°C
R&D / pilot100% hydrogen combustion
Fully commercialised / H₂ readyProcess gas up to 1,700°C
Commercial-scale pilot planned| Electric heater | Plasma torch | H₂ burner | RotoDynamic heater | |
|---|---|---|---|---|
| EAF | – | – | Commercial | Commercial-scale pilot planned |
| Ladle preheating | Commercial | R&D / pilot | Commercial | Commercial-scale pilot planned |
| Reheat furnace | Commercial | R&D / pilot | Commercial | Commercial-scale pilot planned |
| Cleaning / annealing | Commercial | – | Commercial (H₂-ready) | Commercial-scale pilot planned |
How they compare
| Electric heater | Plasma torch | Hydrogen burner | RotoDynamic heater | |
|---|---|---|---|---|
| Where it applies | Ladle preheating, reheating furnaces, annealing | Ladle preheating, reheating furnaces | EAF, ladle preheating, reheat furnace, annealing | EAF, ladle preheating, reheat furnace, annealing |
| Heat and efficiency | Up to 95% thermal efficiency | Plasma jet up to 5,000°C | 100% hydrogen combustion, very high flame temperatures | Process gas up to 1,700°C; roughly 90–95% thermal efficiency |
| Main challenge | Significant grid and electrical upgrades; elements can degrade under thermal shock or oxidation | System energy demand about 25% above gas burners; refractory wear | Shorter flames, flashback and NOx risks that call for redesigned furnaces, nozzles and valves | No prolonged operating data at full industrial scale |
| CAPEX | USD 622,000–5,349,000 per MW | Up to USD 383 per tonne of liquid steel capacity | About 40% of overall furnace CAPEX for a retrofit | Undisclosed |
Electric annealing works at scale. Nordic special steel manufacturer Ovako pioneered the approach in 2014 and has electrified approximately 90% of its heat treatment capacity.
Hydrogen heating is already running. Ovako’s reheating furnace at Hofors and ArcelorMittal’s ladle preheater at Sestao are both powered by green hydrogen.
Three steps for EAF operators
1. Prioritise reheating furnace decarbonisation
Given that reheating furnaces alone account for over 44% of the steelmaking process’s Scope 1 emissions, interventions in this specific process will yield the highest proportional GHG abatement.
2. Champion direct electrification powered by RE
Acknowledging the heavy energy penalties associated with hydrogen electrolysis, direct electrical heating technologies should serve as the primary decarbonisation vector. Electrification must be powered with RE to eradicate subsequent Scope 2 emissions.
3. Investigate mature technologies despite commercial ambiguity
Heating alternatives for every process traditionally reliant on gas burners are technologically mature. Whilst comprehensive economic comparisons are currently hindered by CAPEX ambiguity, EAF operators would benefit from proactively engaging in pilot projects now to validate operational efficiencies and ensure they are positioned to scale as these technologies advance.
Basis: global average emissions and ranges drawn from the public sources listed in the report’s end notes. Energy comparisons use direct heating efficiency, with plasma torch cooling demand adding about 25% to system energy demand. For information only; not investment advice. The report represents the authors’ views and interpretations of publicly available information.